Chemical Storage Container: Safety Standards for Hazardous Materials in Industrial Facilities
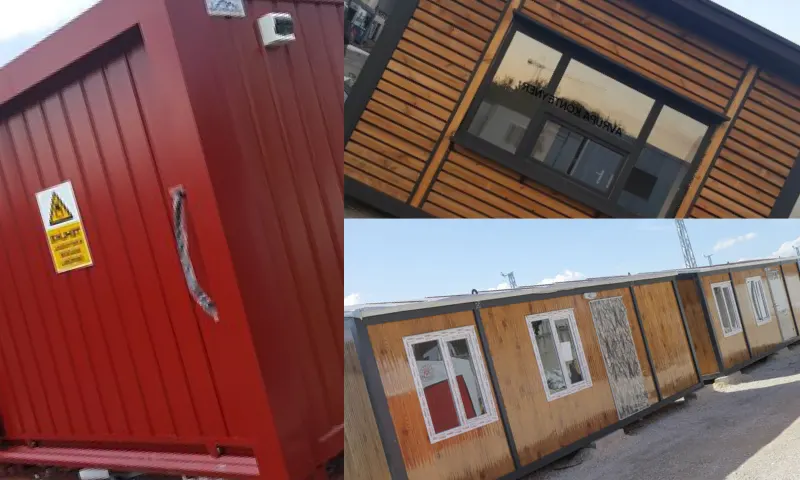
Chemical Storage Container: Leak-Proof Infrastructure, Ex-Proof Equipment, and Insulation
The safe storage of raw materials and waste used in industrial facilities, laboratories, automotive factories, and chemical manufacturing plants is one of the most critical requirements of occupational health and environmental protection legislation. The uncontrolled storage of flammable, combustible, acidic, or toxic chemicals can lead to serious industrial accidents and irreversible environmental disasters. These special modular structures, produced in full compliance with environmental regulations and international safety standards, are designed to minimize leakage and explosion risks. Europe Container, a leading brand in modular construction and industrial storage solutions, offers custom engineering solutions for your facility through its portal at https://avrupakonteyner.com/urunler/kimyasal-depolama-konteyneri. With a certified Chemical Storage Container integrated into your facility, you can store your hazardous materials with high security measures, without falling foul of legal inspections.
Chemical Storage Container: Corporate Procurement Processes and Site Delivery Assurance
The most important factors to consider in the design of a Chemical Storage Container are the selection of materials suitable for the type of chemical and leak prevention engineering. The base sections of the storage units produced by Europe Container are equipped with grated collection pools that capture potential spills and leaks. Ex-proof (explosion-proof) ventilation fans, lighting elements, and gas detection sensors are integrated into the system for the discharge of toxic or flammable gases that may accumulate inside. Depending on your needs, Chemical Storage Container models can be fully customized to your facility's storage requirements with fire-resistant rock wool panel claddings, automatic fire suppression systems, and corrosion-resistant special coating options. When investing in a Chemical Storage Container, not only the product quality but also the assurance that all processes, from manufacturing to on-site installation, are carried out under corporate guarantee is essential. The automated manufacturing process, which begins with the confirmation of your order, undergoes strict quality inspections, is completed within the agreed timeframe, and is dispatched to your facility via special transport vehicles. Our company, operating on the principle of transparent pricing, protects your corporate budget by not incurring surprise costs beyond the initially agreed-upon project cost. Even after sales, we offer professional guidance with our expert technical team, from site preparation to commissioning steps. If you want to eliminate risks and create legally compliant storage areas at your industrial site, you can find solutions with the assurance of Europe Container.